
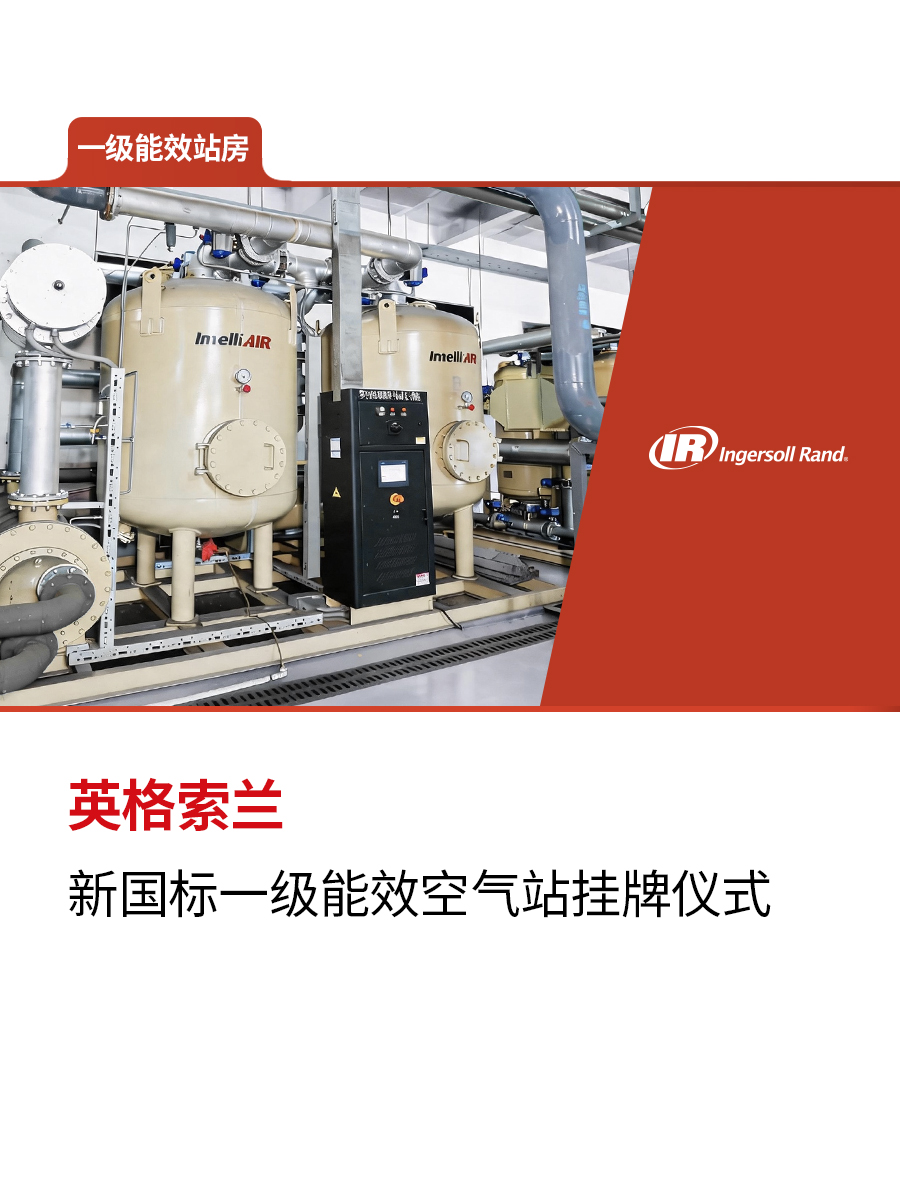
Anhui Highly Precision Casting Co., Ltd. has officially achieved Grade 1 Certification for its Smart Compressed Air Station. Following an independent third-party assessment conducted in accordance with relevant national standards, the project was recognized as meeting China's Grade 1 Compressed Air Station Energy Efficiency Standard.
As a leading example of smart compressed air station development in the casting industry, the project has delivered significant energy savings and carbon reduction while providing manufacturers with a proven model for achieving lower operating costs, higher efficiency, and more sustainable growth through compressed air system upgrades.
The certification not only validates the project's outstanding performance but also marks a new milestone in the collaboration between Anhui Highly and Ingersoll Rand in energy efficiency, smart operations, and sustainable development.
Green Upgrade: Turning Compressed Air into a New Driver of Decarbonization
Anhui Highly Precision Casting Co., Ltd. has long specialized in the manufacture of components for compressors, automotive applications, and rail transportation systems.
As its business continued to expand, compressed air demand increased steadily, and the existing air system began to face challenges including aging equipment, high energy consumption, and insufficient supply stability.
As one of the most critical utility systems in manufacturing, the efficiency of a compressed air system directly impacts operating costs, production reliability, and sustainability performance.
Driven by its long-term commitment to green manufacturing and sustainable development, Anhui Highly launched a comprehensive compressed air system upgrade project and partnered with Ingersoll Rand to develop a Grade 1 Smart Compressed Air Station. Through more efficient and intelligent energy management, the project supports energy conservation, operational optimization, and the company's continued high-quality development.
From Equipment Upgrades to Smart Operations
Based on the customer's production characteristics, compressed air demand patterns, and future development requirements, Ingersoll Rand designed a customized end-to-end solution that integrates high-efficiency equipment, intelligent control, and digital management technologies to enhance both system efficiency and reliability.
The project combines NX Series centrifugal compressors with ESM Series variable-speed rotary screw compressors, supported by high-efficiency air treatment equipment and powered by the iControl intelligent control system and cloud platform.
This integrated solution enables:
· Real-time equipment monitoring
· Energy performance analysis
· Intelligent multi-compressor coordination
· Predictive maintenance
Through intelligent multi-compressor control and dynamic optimization, the system automatically adjusts operating strategies according to actual compressed air demand, ensuring stable air supply while continuously maximizing energy efficiency.
The project represents a transformation from traditional equipment-focused management to data-driven smart operations.
Delivering Measurable Results
Since commissioning, the compressed air system has achieved substantial improvements in efficiency, reliability, and digital management:
✅ Approximately 20% reduction in overall energy consumption
✅ More than 3 million kWh of electricity saved annually
✅ Annual energy cost savings exceeding RMB 2 million
✅ Approximately 2,110 tonnes of CO₂ emissions reduced per year
✅ Significantly improved air supply reliability, supporting uninterrupted production
✅ 24/7 cloud-based monitoring and predictive maintenance, reducing operating costs and equipment risks
These achievements provide not only measurable energy savings but also a more stable, efficient, and intelligent energy management framework that will continue creating long-term value for the business.
Industry Recognition
A Benchmark Project Earns Broad Recognition
Industry experts and project stakeholders gathered to celebrate the achievement and highly praised the project's results.
Dr. Wang Yikai
Committee Member, Compressed Air Station Energy Efficiency Rating Group, China Energy Conservation Association
Lecturer, Hehai University
"The Anhui Highly Grade 1 Smart Compressed Air Station is an outstanding example of how the casting industry can implement China's carbon reduction objectives while improving energy performance. The project effectively addresses challenges commonly found in traditional compressed air stations, including excessive energy consumption and inefficient management practices. It provides a scalable and replicable model for industrial energy-efficiency upgrades and will continue driving regional green and low-carbon development."
Mr. Miao Jianhui
General Manager, Anhui Highly Precision Casting Co., Ltd.
"The performance of the Smart Compressed Air Station has exceeded our expectations and delivered tangible benefits in both energy savings and operational efficiency. Ingersoll Rand's technical expertise and service capabilities have proven highly reliable. We look forward to further cooperation in areas such as heat recovery and additional energy-efficiency initiatives."
Mr. Ma Kejun
Head of Safety and Environmental Management, Anhui Highly Precision Casting Co., Ltd.
"The successful implementation of the Smart Compressed Air Station has significantly supported our sustainability objectives and low-carbon transformation efforts. The stable and efficient compressed air supply has improved operational reliability while reducing maintenance costs. We look forward to expanding our collaboration with Ingersoll Rand in energy management and operational excellence."
Mr. Guo Lei
National Sales Leader, Smart Integrated Energy Business, Ingersoll Rand
"This project further strengthened our expertise in compressed air system optimization for precision casting and machining industries. Going forward, Ingersoll Rand will continue working closely with Anhui Highly to explore new opportunities for energy savings and carbon reduction while creating additional benchmark projects for the industry."
A Model for Sustainable Manufacturing
The successful certification of the Anhui Highly Grade 1 Smart Compressed Air Station represents far more than a single project achievement.
It demonstrates an important transition within manufacturing, from equipment-level energy savings to system-level optimization, and from isolated improvements to intelligent energy management.
Through equipment upgrades, intelligent multi-compressor control, digital management, and continuous optimization, the project successfully achieved:
· Lower energy consumption
· Stable and reliable compressed air supply
· Intelligent system management
· Improved operational performance
For industries with high compressed air demand, including casting, machining, automotive components, and home appliance manufacturing, the project clearly shows that a systematic and intelligent compressed air station upgrade can simultaneously reduce energy consumption, lower operating costs, improve production reliability, and strengthen energy management capabilities.
Anhui Highly's success provides a proven, scalable model for manufacturers seeking to build Grade 1 Energy-Efficient Compressed Air Stations and accelerate their own green transformation journeys, while contributing to broader carbon reduction objectives across the industry.
Moving Toward a Greener Future Together
The successful certification of Anhui Highly's Grade 1 Smart Compressed Air Station once again demonstrates the critical role that high-efficiency compressed air systems play in industrial sustainability and green transformation.
Looking ahead, Ingersoll Rand will continue leveraging its expertise in compressed air systems, intelligent controls, and energy management to help manufacturers build more efficient, sustainable, and intelligent utility infrastructures.
By applying proven best practices and scalable solutions across industries, Ingersoll Rand will continue helping customers reduce energy consumption, lower carbon emissions, cut operating costs, and achieve long-term sustainable growth, contributing to a greener, smarter, and more sustainable industrial future.